



Aging Room vs. Constant Temperature Room: Key Differences
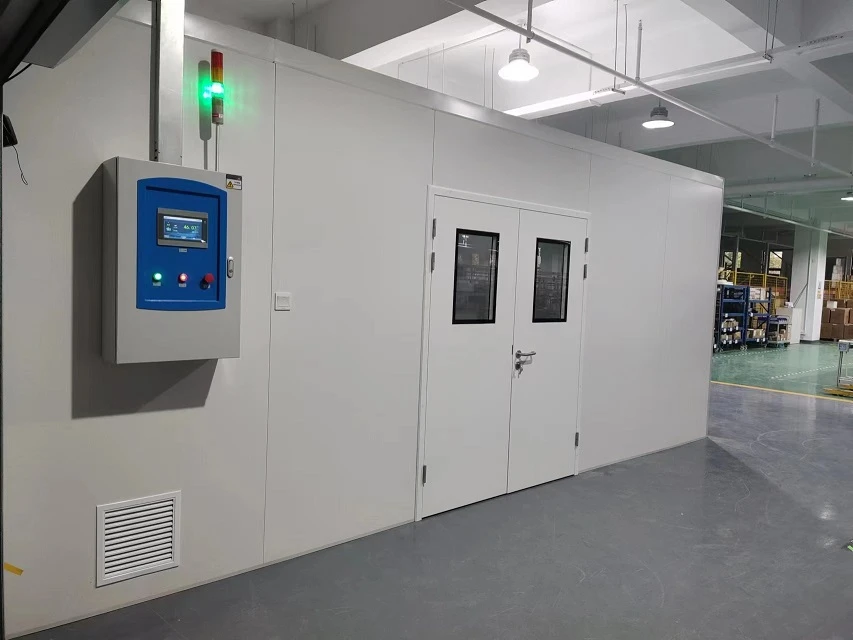
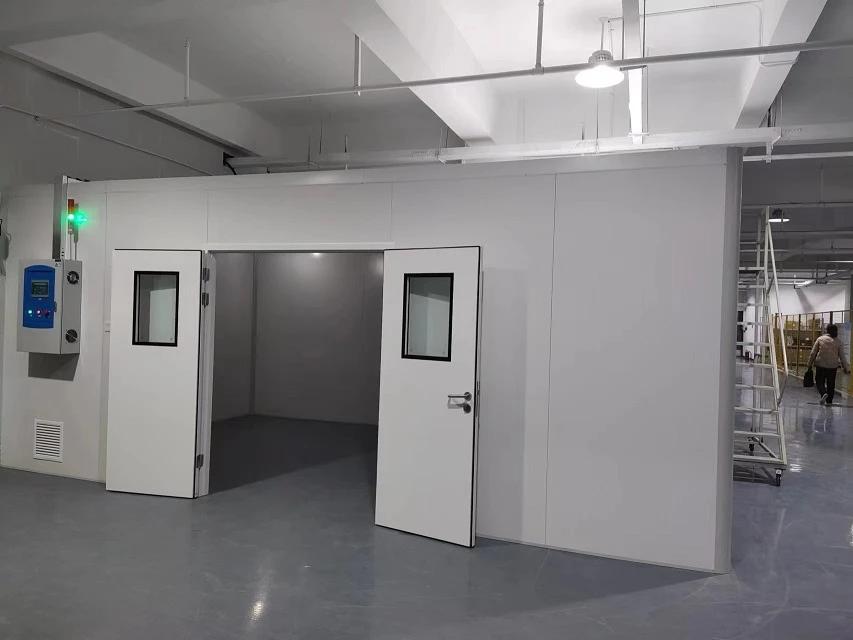
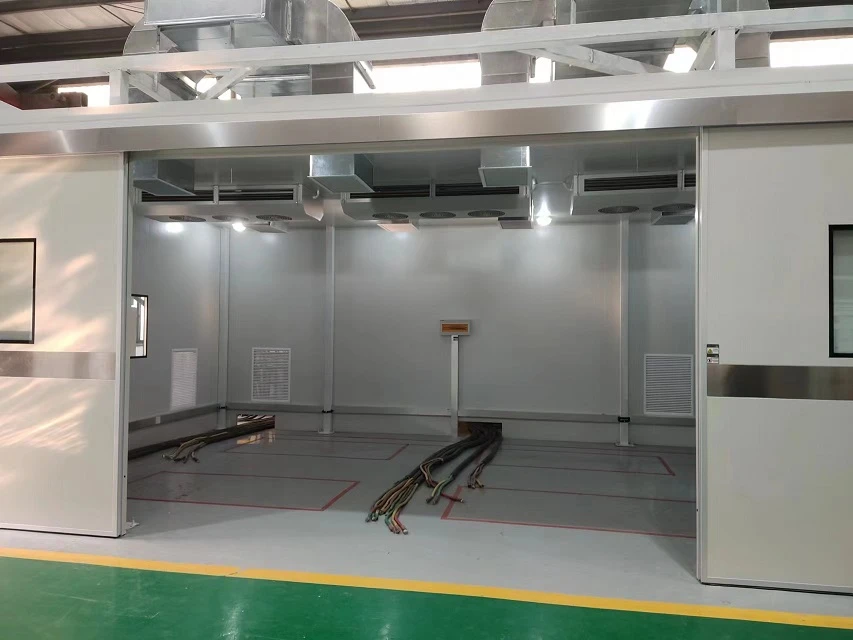
Selecting a qualified environmental test chamber is critical for electronics manufacturing reliability validation. ALP Technology's walk-in aging room (burn-in room) executes accelerated life testing for PCBA subassemblies and finished electronic units, screening out infant mortality failures and enhancing long-term operational reliability.
Static burn-in subjects DUTs (devices under test) to elevated temperature without power excitation, while dynamic burn-in energizes the DUTs to emulate real-life operational profiles. Dynamic burn-in enables rapid defect screening within a 4-hour stress cycle. The ALP aging room supports a temperature envelope from ambient temperature (RT) up to 85°C. For PCBA burn-in validation, the typical setpoint is 85°C ±2°C. For complete end-products, testing is recommended below 50°C or 60°C, as their nominal operating window ranges from ambient to 40°C. Elevated temperature beyond the product's design limit drives unnecessary capital and operational overhead without tangible reliability gain. Preparatory infrastructure including burn-in racks, contact sockets, signal harnesses, electronic loads, and digital traceability systems must be deployed prior to test execution.
ALP Technology's constant temperature room delivers controlled ambient conditioning for weathering resistance assessment, material curing, precision component storage, microbiological incubation, and temperature stability verification for pharmaceuticals, beverages, dairy and food commodities. Its calibrated operating range is 0~40°C (±2°C), engineered to replicate natural outdoor ambient conditions. An active refrigeration subsystem maintains thermal stability when external ambient temperature exceeds the target setpoint.
In summary, ALP aging rooms are purpose-built for high-temperature accelerated burn-in stress screening, whereas ALP constant temperature rooms are optimized for near-ambient conditioning applications. The core differentiator lies in their designed temperature envelope and thermal stress capability.

ALP Technology: One-Stop Customized Test Chamber Solutions
Different from ordinary standard testing equipment, ALP Technology focuses on independent R&D, production and customization of environmental test chambers. With core advantages of high precision, strong stability, diverse simulation functions and flexible personalized customization, our products cover constant temperature and humidity test chambers, thermal shock test chambers, high-altitude low-pressure test chambers, aging test chambers and other full-series products. Targeting the differentiated testing demands of various industries, ALP Technology provides one-stop professional testing solutions for global enterprises and research institutions, helping customers improve product quality, shorten R&D cycles, and gain market competitive advantages.
Whether you are standardizing a new product line or solving a difficult failure issue, ALP TECHNOLOGY is ready to help.
✉️ E-mail: info@alp-environment.com
🔗 Website: www.alp-environment.com
"Technological Excellence Rooted in Integrity" - engineered into every test, delivered with every partnership.